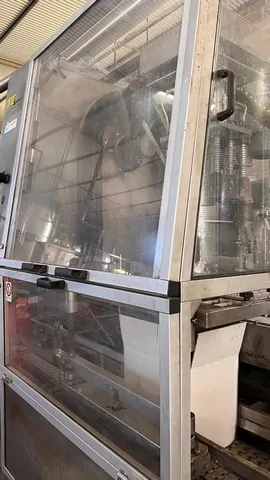
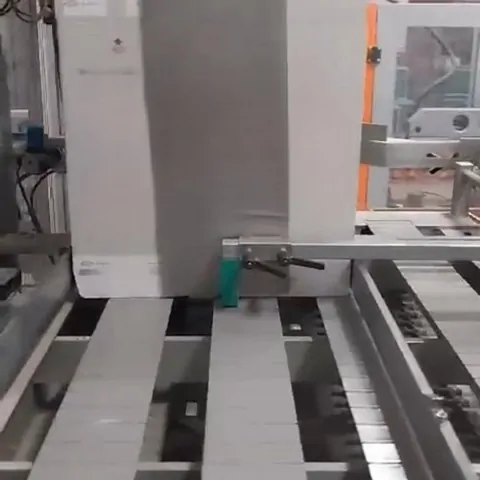
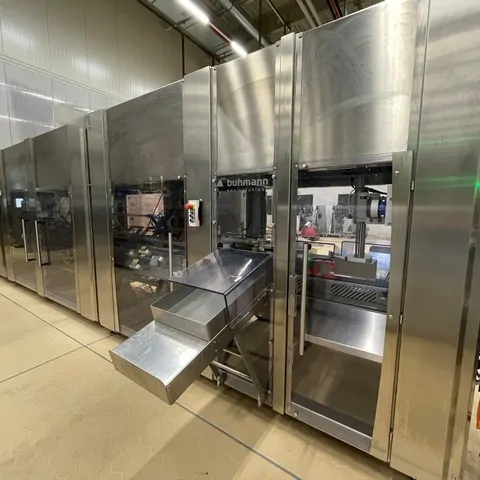
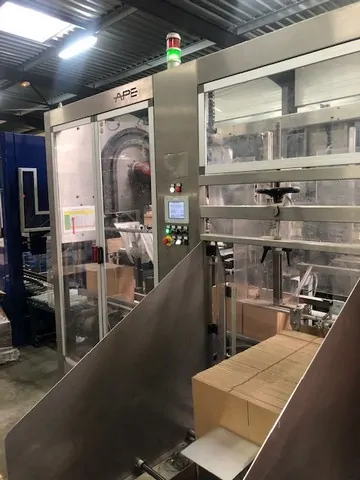
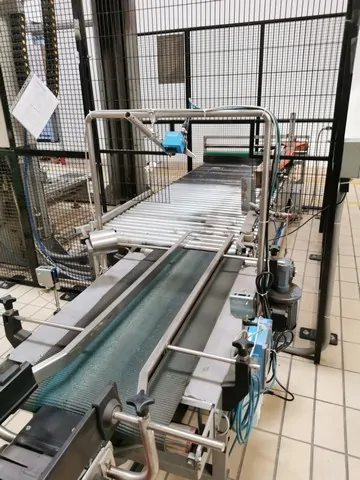
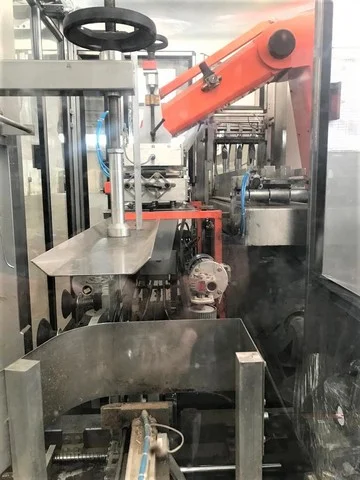
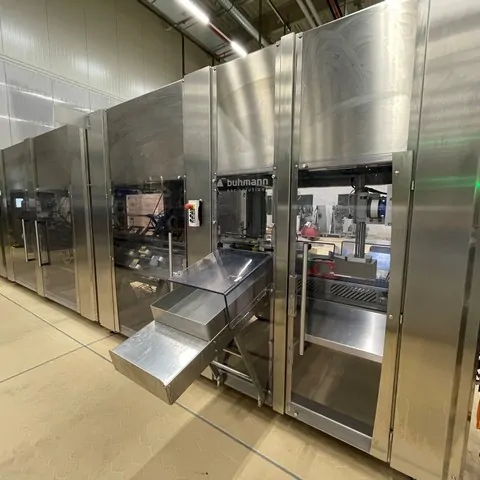


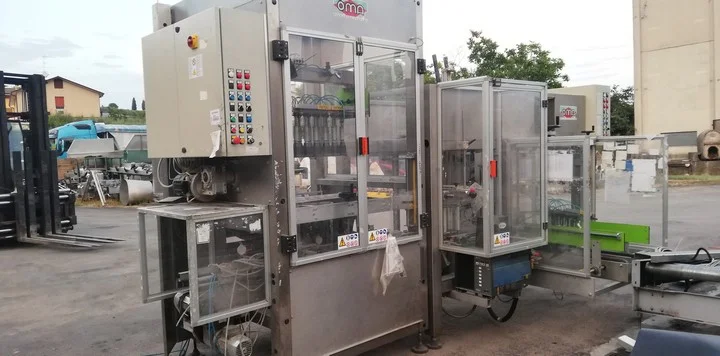
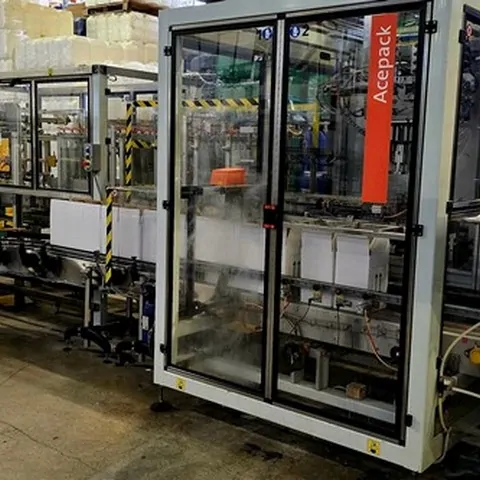

Used Case Packing Monoblocks
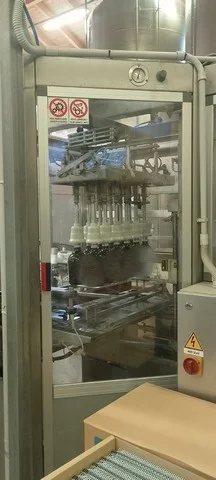
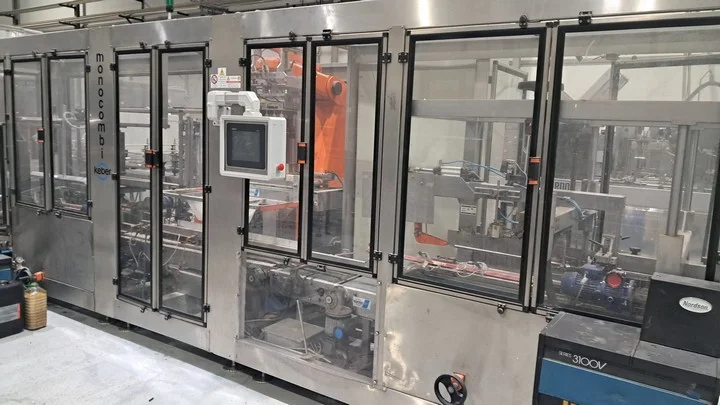
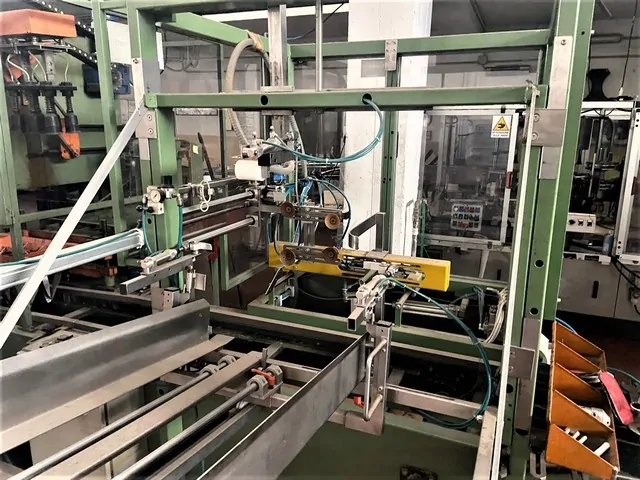
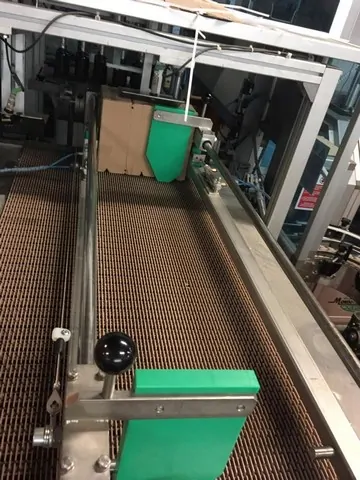
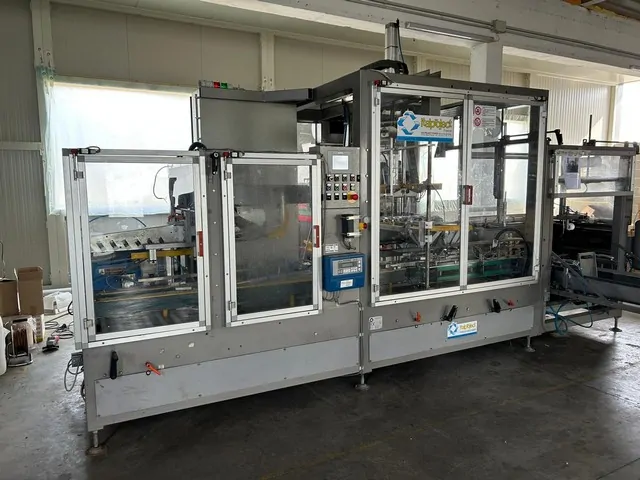
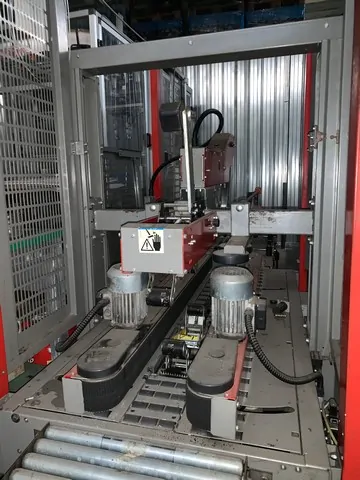
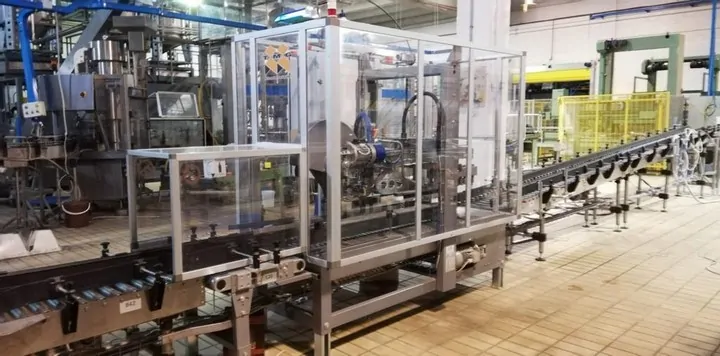
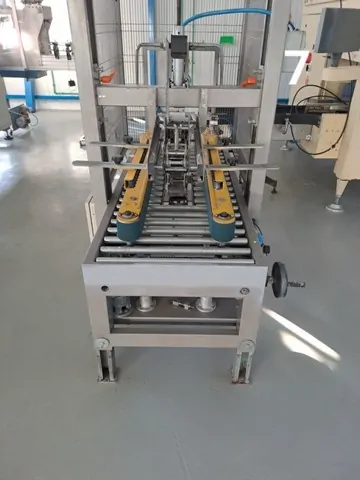
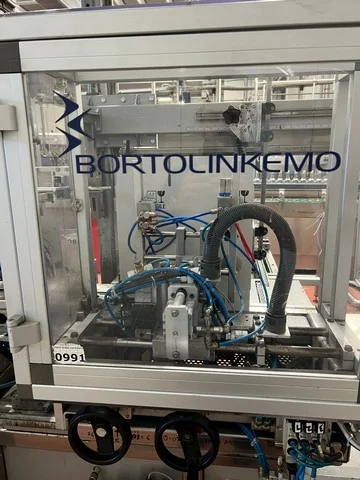
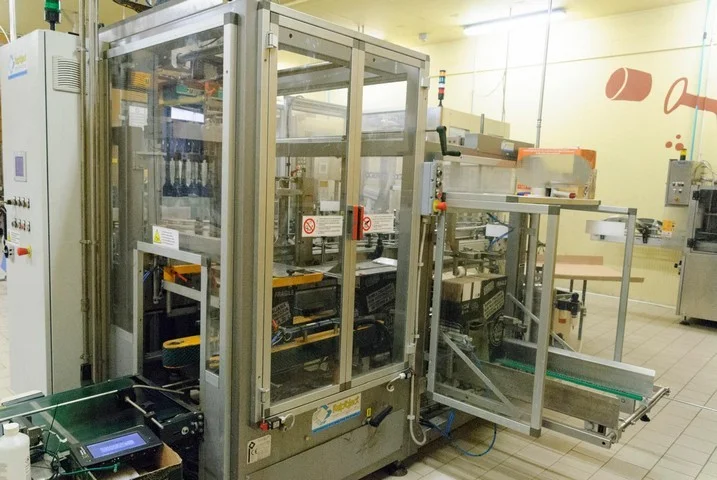
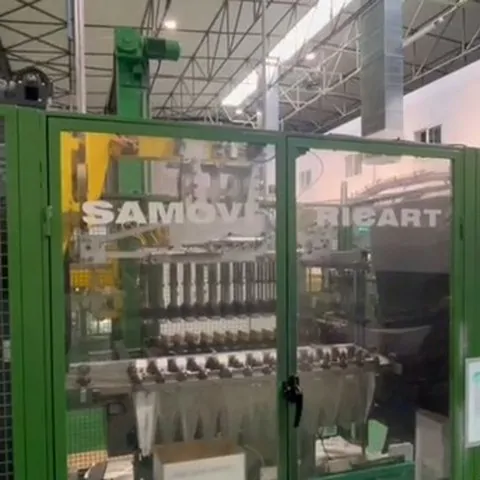
Case-packing monoblocks combine multiple secondary-packaging operations in one integrated machine or compact platform. Depending on the model, they may erect cases or trays, collate products, load the package and close or seal it.
Why Monoblock Architecture Matters
Integrated architecture reduces transfers between separate machines and can simplify synchronization, but it also means format compatibility and included tooling must be evaluated as a complete system.
What to Check Before Buying
Confirm product type, bottle or can dimensions, case style, pack pattern and board specification. Check loading mechanism, case-forming section, hot-melt or tape unit, servo axes, grippers, conveyors, safety system, PLC and change parts.
Integration
Verify infeed and discharge height, nominal production direction, available accumulation and the communication interface with upstream labelling or shrink wrapping and downstream palletizing.
Applications
These machines are used where floor space is limited or where a compact, synchronized end-of-line packaging cell is preferred.